Why coating and cathodic protection reinforce each other
A common misconception is that a good coating makes cathodic protection unnecessary, or conversely, that cathodic protection can replace a properly designed coating system. In reality, the two systems reinforce each other. A coating forms the first physical barrier between the steel and the electrolyte. Cathodic protection then provides active protection at locations where the coating is damaged, aged or imperfect.
For buried and submerged steel structures, combining both methods is therefore often the most reliable and economical solution.
A good coating reduces current demand
Cathodic protection only needs to supply current to the areas of steel that are electrically in contact with the electrolyte. The better the coating, the smaller the actively exposed surface area and the lower the required protection current.
This has direct advantages for the sizing of the CP system:
- lower rectifier power requirements;
- fewer or smaller anodes;
- lower anode consumption;
- longer system life;
- lower investment and operating costs.
The design therefore takes into account the expected condition and degradation of the coating over the full service life of the installation. A good coating does not make cathodic protection redundant; it makes it more efficient.
Why coating alone is not enough
No coating system can be guaranteed to remain completely defect-free for decades. Damage can occur during transport, installation, backfilling, maintenance activities or simply due to ageing. Even small pinholes or local defects can be sufficient to expose the steel directly to the electrolyte.
In the presence of stray currents, such small defects can become particularly critical. When almost the entire steel surface is electrically insulated by the coating, an external direct current can only pass between the steel and the electrolyte through a limited number of defects.
Locations where current leaves the steel and enters the electrolyte are particularly critical. This is where anodic metal dissolution occurs. The smaller the available current discharge area, the higher the local current density can become.
As a result, a very small coating defect can locally experience a much higher corrosion rate than a large, uniformly exposed steel surface.
Faraday makes the risk tangible
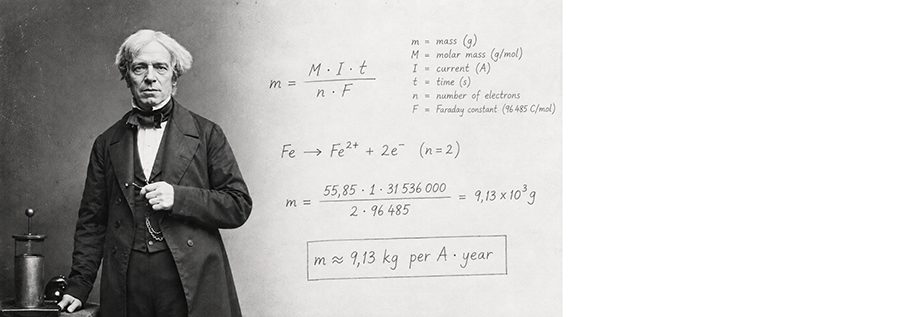
The relationship between electrical current and metal loss follows from Faraday’s law.
For iron dissolving anodically as Fe²⁺, a continuous anodic current of:
1 A for one year corresponds to approximately 9.13 kg of iron loss.
This does not mean that every ampere flowing through a pipeline automatically causes this amount of corrosion. It specifically refers to anodic current leaving the steel and entering the electrolyte.
The area over which that current is distributed then determines how concentrated the metal loss will be. If the same current is discharged through a single small coating defect, a very high local corrosion rate can develop.
This is precisely why a good coating alone does not provide complete protection against electrical interference or localized corrosion.
Coating and cathodic protection complement each other!
The functions of both systems are different, but complementary:
A coating minimizes contact between the steel and the electrolyte. Cathodic protection protects the steel wherever such contact still occurs.
The coating therefore reduces the required protection current, while cathodic protection compensates for the unavoidable weak points and future degradation of the coating. For critical buried and submerged steel structures, this combination forms the basis of a robust, efficient and durable corrosion protection strategy.